PHARMACEUTICAL INDUSTRY

High-performance thermoplastic pumps for the pharmaceutical industry

Engineered for absolute containment and zero-contamination transfer of active
pharmaceutical ingredients (APIs) and fine chemicals.

High purity fluid handling

Pumping solutions for critical and high-purity processes

Synthesizing medicines and processing fine chemicals demand strict adherence to the most stringent regulatory and safety standards in the world. When transferring high-value active pharmaceutical ingredients (APIs) or managing aggressive cleaning reagents, your facility requires equipment that guarantees absolute containment and zero product contamination.

Tecnium Pumps engineers specialized thermoplastic fluid handling systems designed exclusively for these sterile environments. Manufactured from virgin, solid-block polymers such as PVDF and E-CTFE, our equipment offers absolute resistance to chemical attack, ensuring continuous, safe, and highly efficient operation while protecting your delicate formulations from any risk of metallic degradation.
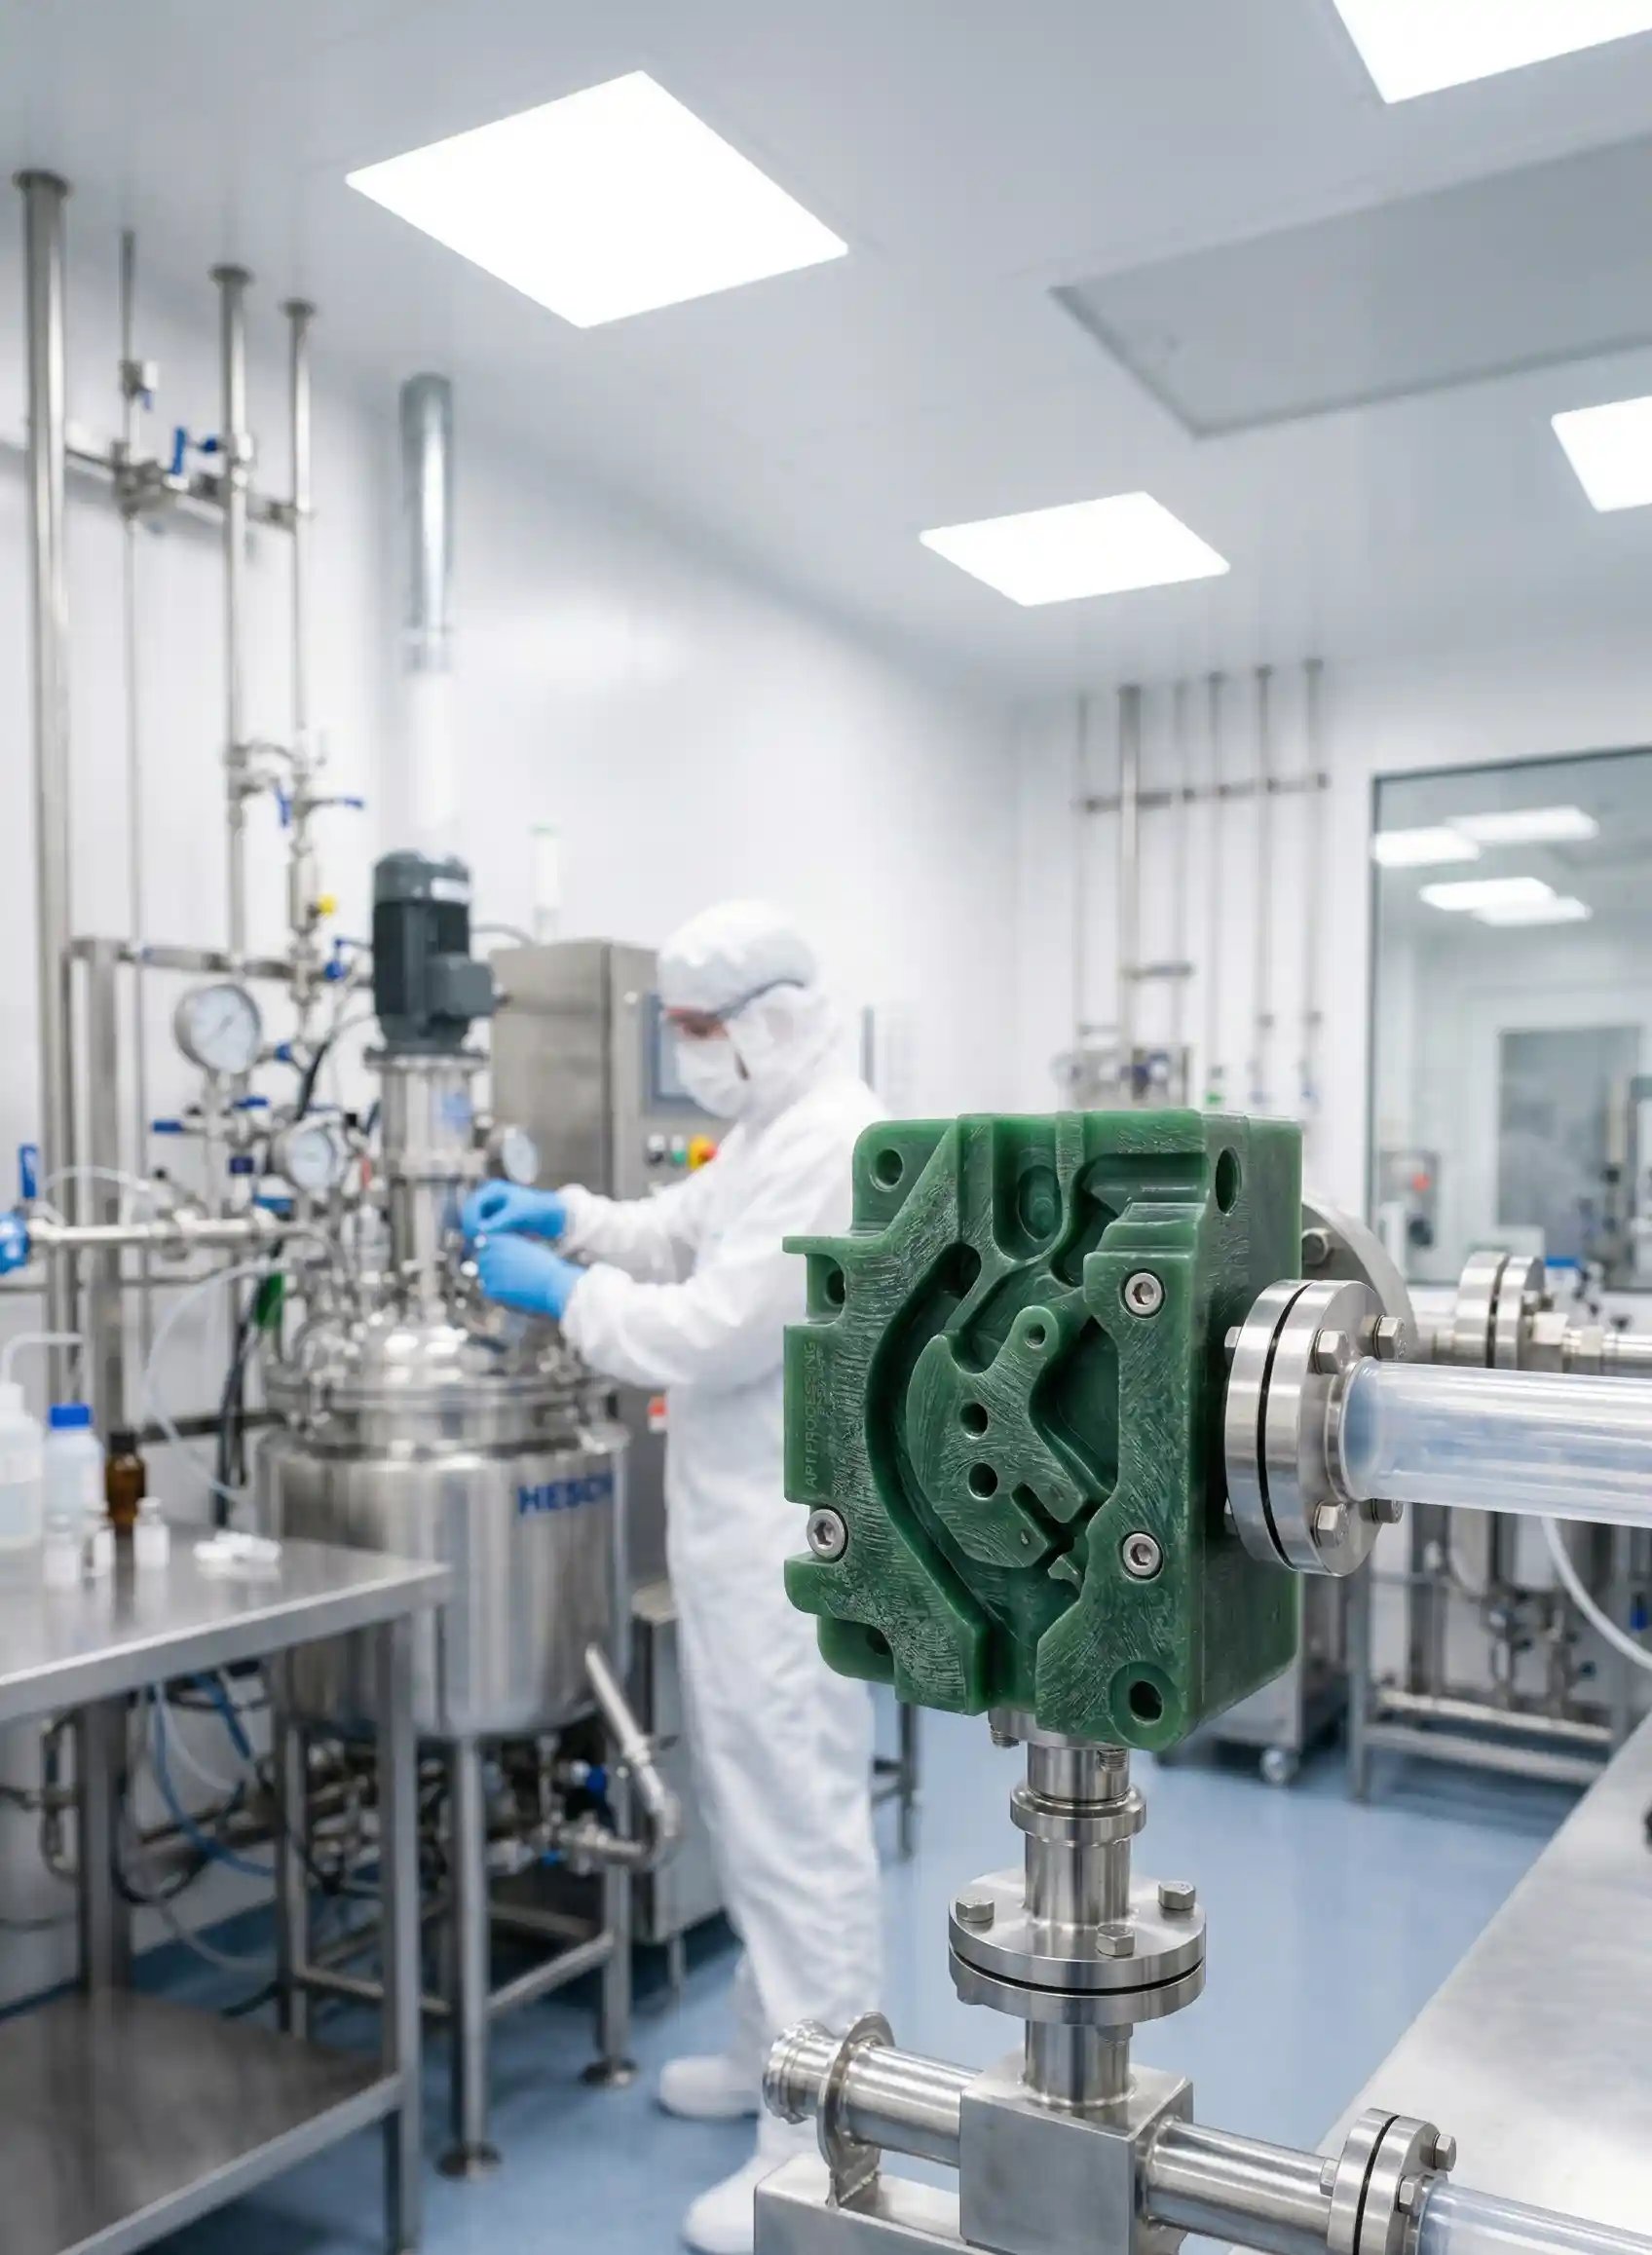
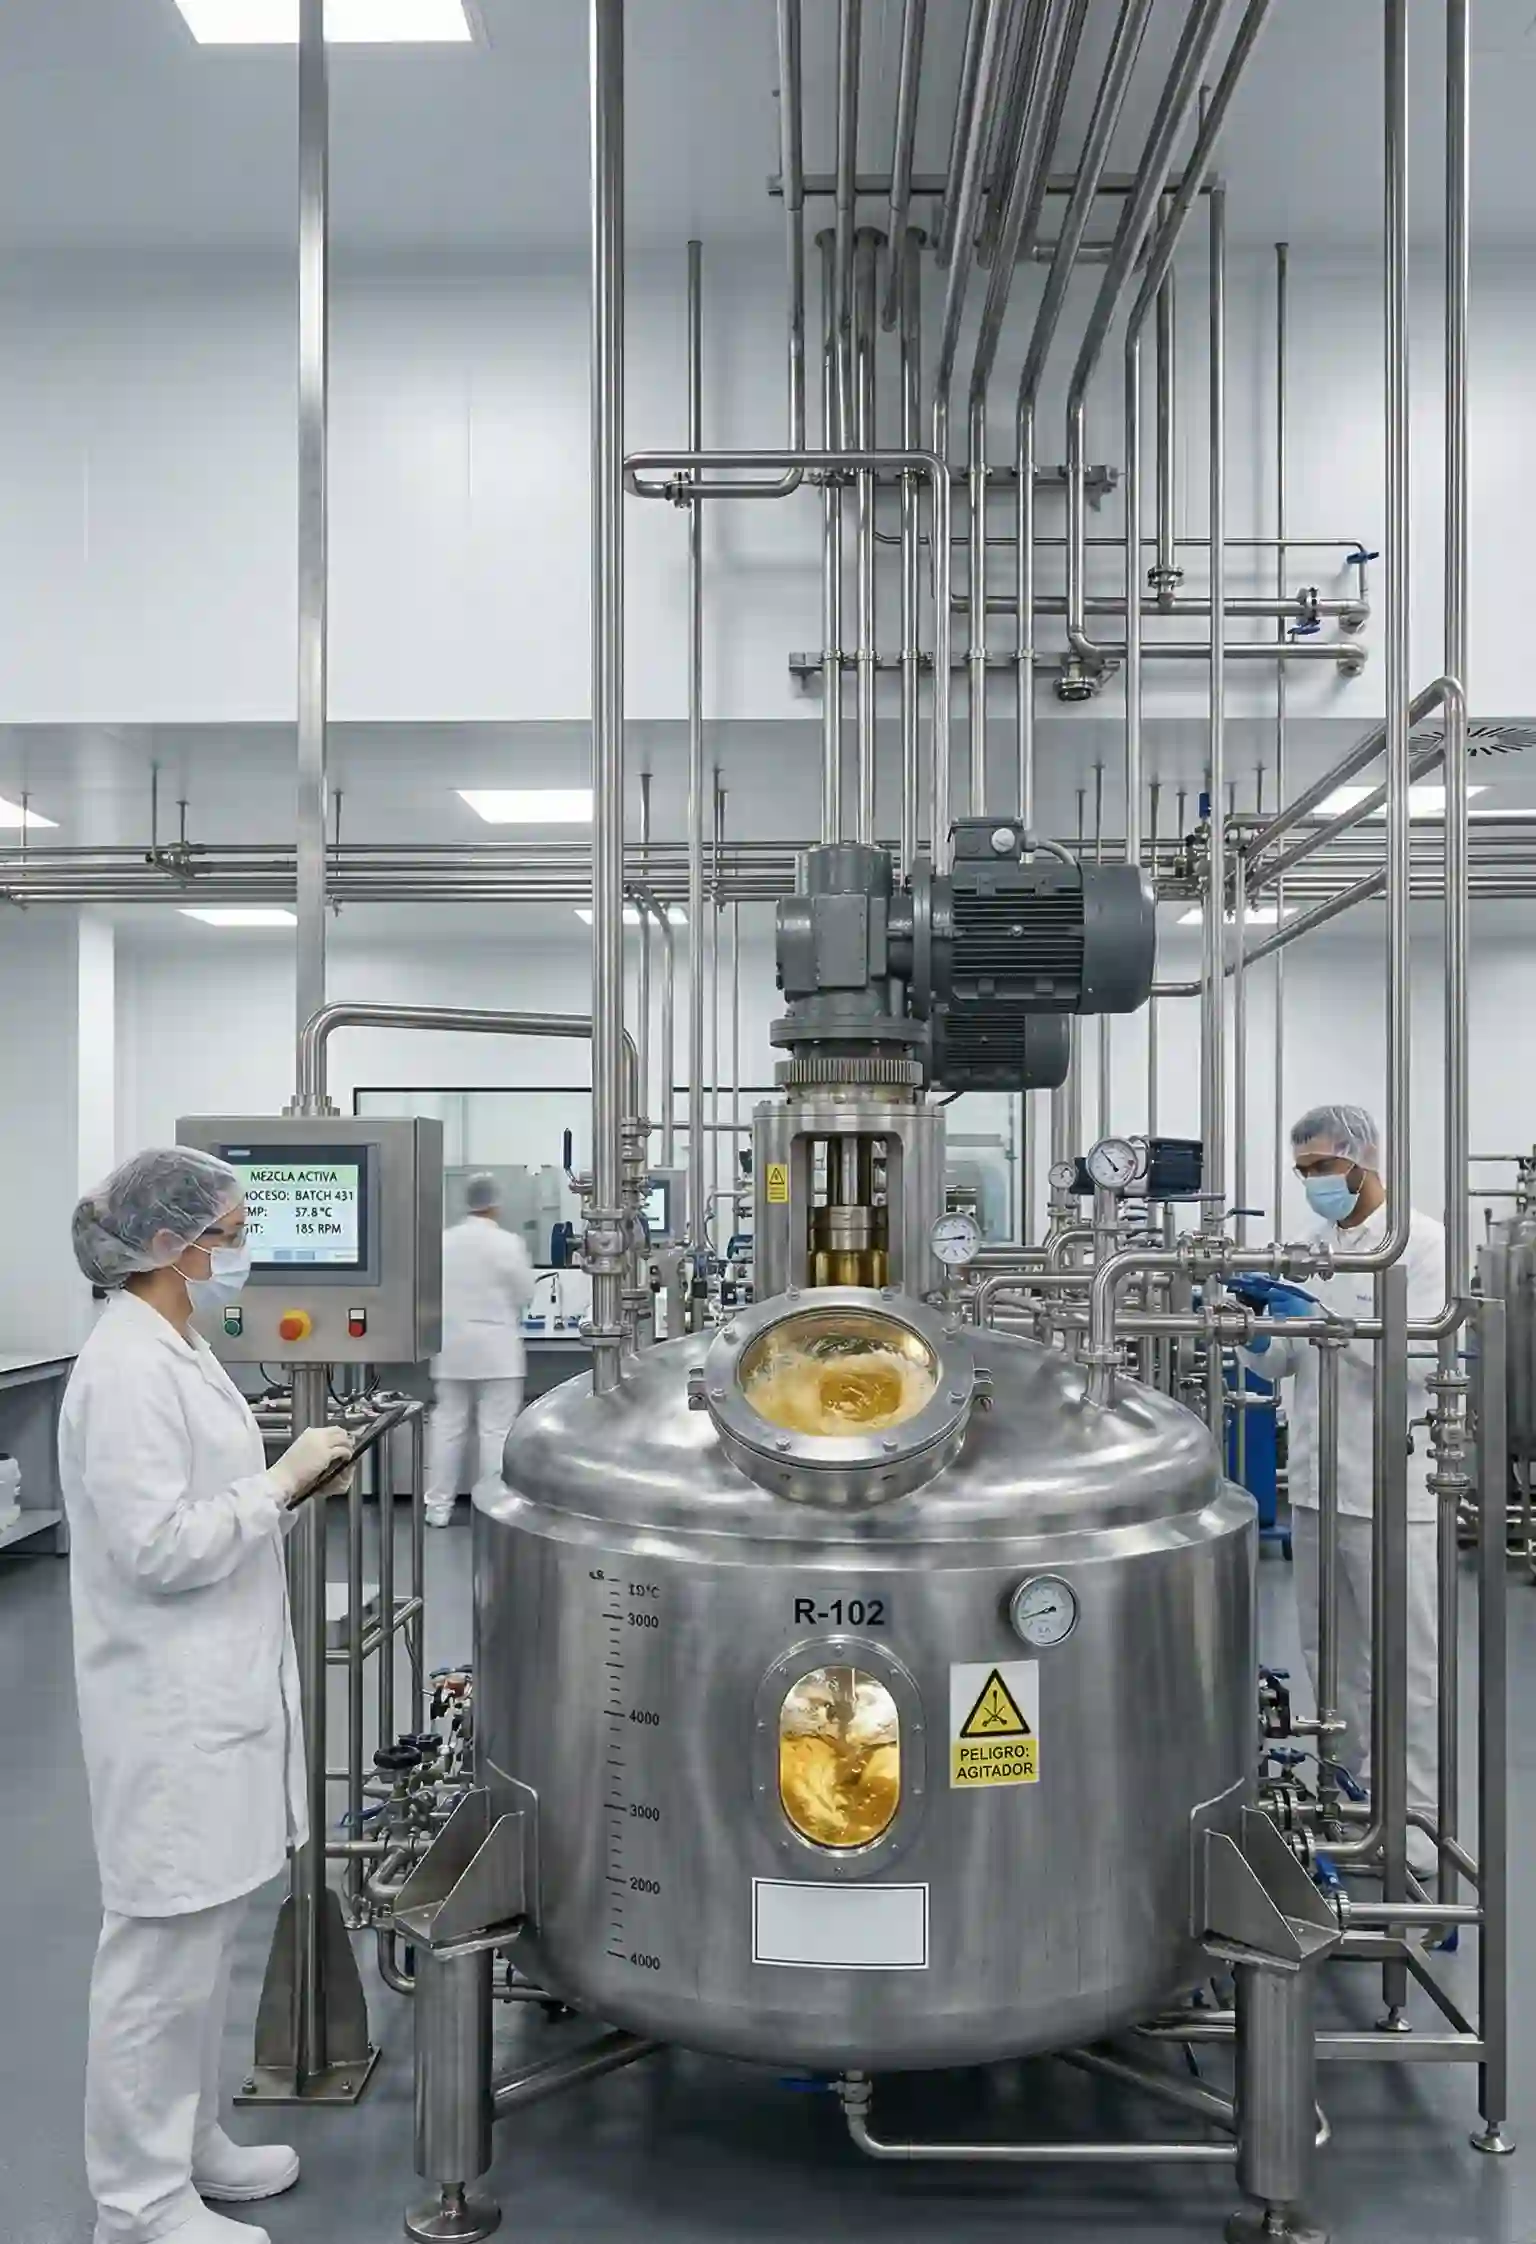
pharmaceutical pumping solutions
Pharmaceutical industry

Designed for maximum purity

Core benefits for cleanroom and laboratory environments

  • Uncompromised process integrity: Machined from ultra-pure plastics like PVDF and E-CTFE, our pumps eliminate metallic leaching, ensuring your sensitive active ingredients remain entirely uncontaminated.

  • Hermetic isolation technology: Advanced sealless magnetic drive architecture prevents fugitive emissions, safeguarding both your plant operators and the strict sterile conditions of your facility.

  • Optimized for batch production: The exceptionally smooth internal surfaces of our solid thermoplastics resist biological buildup, allowing for rapid and effective flushing between different product runs.

  • Certified protection for volatile solvents: Specialized conductive plastic configurations with full ATEX certification guarantee the risk-free transfer of highly flammable alcohols and reagents used in drug synthesis.

High-performance equipment

Recommended pumping solutions for the pharmaceutical industry

Discover our advanced thermoplastic pump configurations, precision-engineered to safeguard product integrity and maintain sterile conditions in cleanroom environments.

Engineered specifically for the transfer of high-value active ingredients and hazardous solvents. The hermetic isolation shell guarantees absolute zero-leakage performance, safeguarding cleanrooms from contamination while providing essential dry-run protection during batch transfers.

Built for reliable fluid management in fine chemical synthesis. These standardized units eliminate the risk of product degradation caused by metallic corrosion, delivering exceptional purity and stable hydraulic efficiency across demanding pharmaceutical applications.

Designed for tight laboratory environments and mobile process skids. Their compact, direct-coupled architecture requires no mechanical alignment, ensuring rapid installation and the safe handling of sensitive chemical reagents.

The perfect solution for managing biological waste and highly corrosive laboratory effluents. By utilizing a hydrodynamic seal instead of vulnerable mechanical components, they effortlessly handle particle-laden fluids without wearing out.

Built to operate directly inside neutralization tanks and underground wastewater pits. The absence of submerged bearings ensures maximum reliability and totally safe dry-running when emptying chemical waste from pharmaceutical facilities.

Frequently asked questions about our pumps for chemical industry

In critical pharmaceutical synthesis, even microscopic traces of metallic leaching can compromise an entire batch of medication. Standard stainless steel equipment, when exposed to certain cleaning agents or aggressive APIs, is vulnerable to surface degradation. By manufacturing our pumps from solid blocks of ultra-pure thermoplastics like PVDF and E-CTFE, we provide an entirely inert fluid path.

This guarantees that your sensitive products remain completely free from cross-contamination, ensuring full compliance with the strictest industry purity standards.

Unlike lined or coated metal pumps that can chip or flake over time, the homogenous solid plastic construction ensures consistent performance and absolute chemical neutrality throughout the entire lifecycle of the equipment.

Maintaining the integrity of a pharmaceutical cleanroom requires eliminating any potential source of fugitive emissions. Conventional pumps rely on mechanical seals, which inherently require a microscopic fluid film to operate and are always at risk of sudden failure. Our BKM series utilizes advanced magnetic coupling technology, replacing the traditional mechanical seal with a robust, static thermoplastic shell.

This creates a 100% hermetic barrier between the process fluid and the outside atmosphere, making it physically impossible for liquids or hazardous vapours to escape.

By providing absolute containment for volatile solvents and toxic compounds, these pumps safeguard your operators, prevent expensive product loss, and ensure your facility easily passes the most stringent environmental audits.

Absolutely. The production of fine chemicals and active pharmaceuticals often requires the extensive use of highly flammable alcohols and volatile organic compounds (VOCs). Operating standard plastics in these areas poses a severe static discharge risk. To comply with rigorous safety protocols, we manufacture specialized ATEX-certified pump versions using conductive thermoplastic compounds.

Paired with appropriately rated explosion-proof motors, these units safely dissipate static electricity, completely preventing sparks and electrostatic ignition.

This specialized engineering allows our equipment to be securely installed in highly classified hazardous areas (Zone 1 and Zone 2), delivering both the chemical resistance of plastics and the uncompromised safety required by European directives.

Pumping waste streams that contain biological matter, pill coatings, or suspended solids can quickly destroy standard pump seals. For these demanding waste management applications, we engineer vertical cantilever and overflow pumps that completely remove the mechanical seal from the equation.

Because there are no rubbing parts in contact with the abrasive effluent, these specialized units suffer virtually no mechanical wear, drastically reducing your maintenance interventions.

Furthermore, this glandless design means the pumps can run dry safely without any thermal damage, making them incredibly dependable for unpredictable sump drainage, effluent neutralization, and continuous wastewater transfer operations.

Yes, modifying existing pipework in a validated pharmaceutical facility is incredibly expensive and time-consuming. To prevent this, our core industrial ranges are designed to perfectly match globally recognized dimensional norms. They are constructed in strict accordance with the ISO 2858 international standard, guaranteeing precise footprint and flange dimensions.

This precise engineering means that if you need to upgrade an underperforming metallic pump to our high-purity thermoplastic solution, the new unit will drop exactly into the existing footprint without requiring pipe modifications.

This plug-and-play capability drastically reduces installation time, minimizes costly plant downtime, and simplifies your inventory management by standardizing your pumping assets.

Get in touch today

Receive your free quote