Advanced fluid handling

High-performance thermoplastic pumps for the chemical industry

Engineered for the safe and reliable transfer of highly corrosive acids,
alkalis, and abrasive chemical fluids.

Heavy chemical processing

Pumping solutions for highly corrosive and aggressive fluids

The chemical industry demands robust and reliable equipment capable of withstanding the most aggressive operating conditions. Handling strong acids, alkalis, and volatile solvents requires pumping solutions that will not degrade, leak, or fail over time.

Tecnium Pumps designs and manufactures heavy-duty thermoplastic centrifugal pumps specifically for these extreme environments. By utilizing solid-block plastics such as PP, PVDF, and E-CTFE, our pumps offer absolute resistance to chemical attack, ensuring continuous, safe, and highly efficient operation across your entire processing plant.
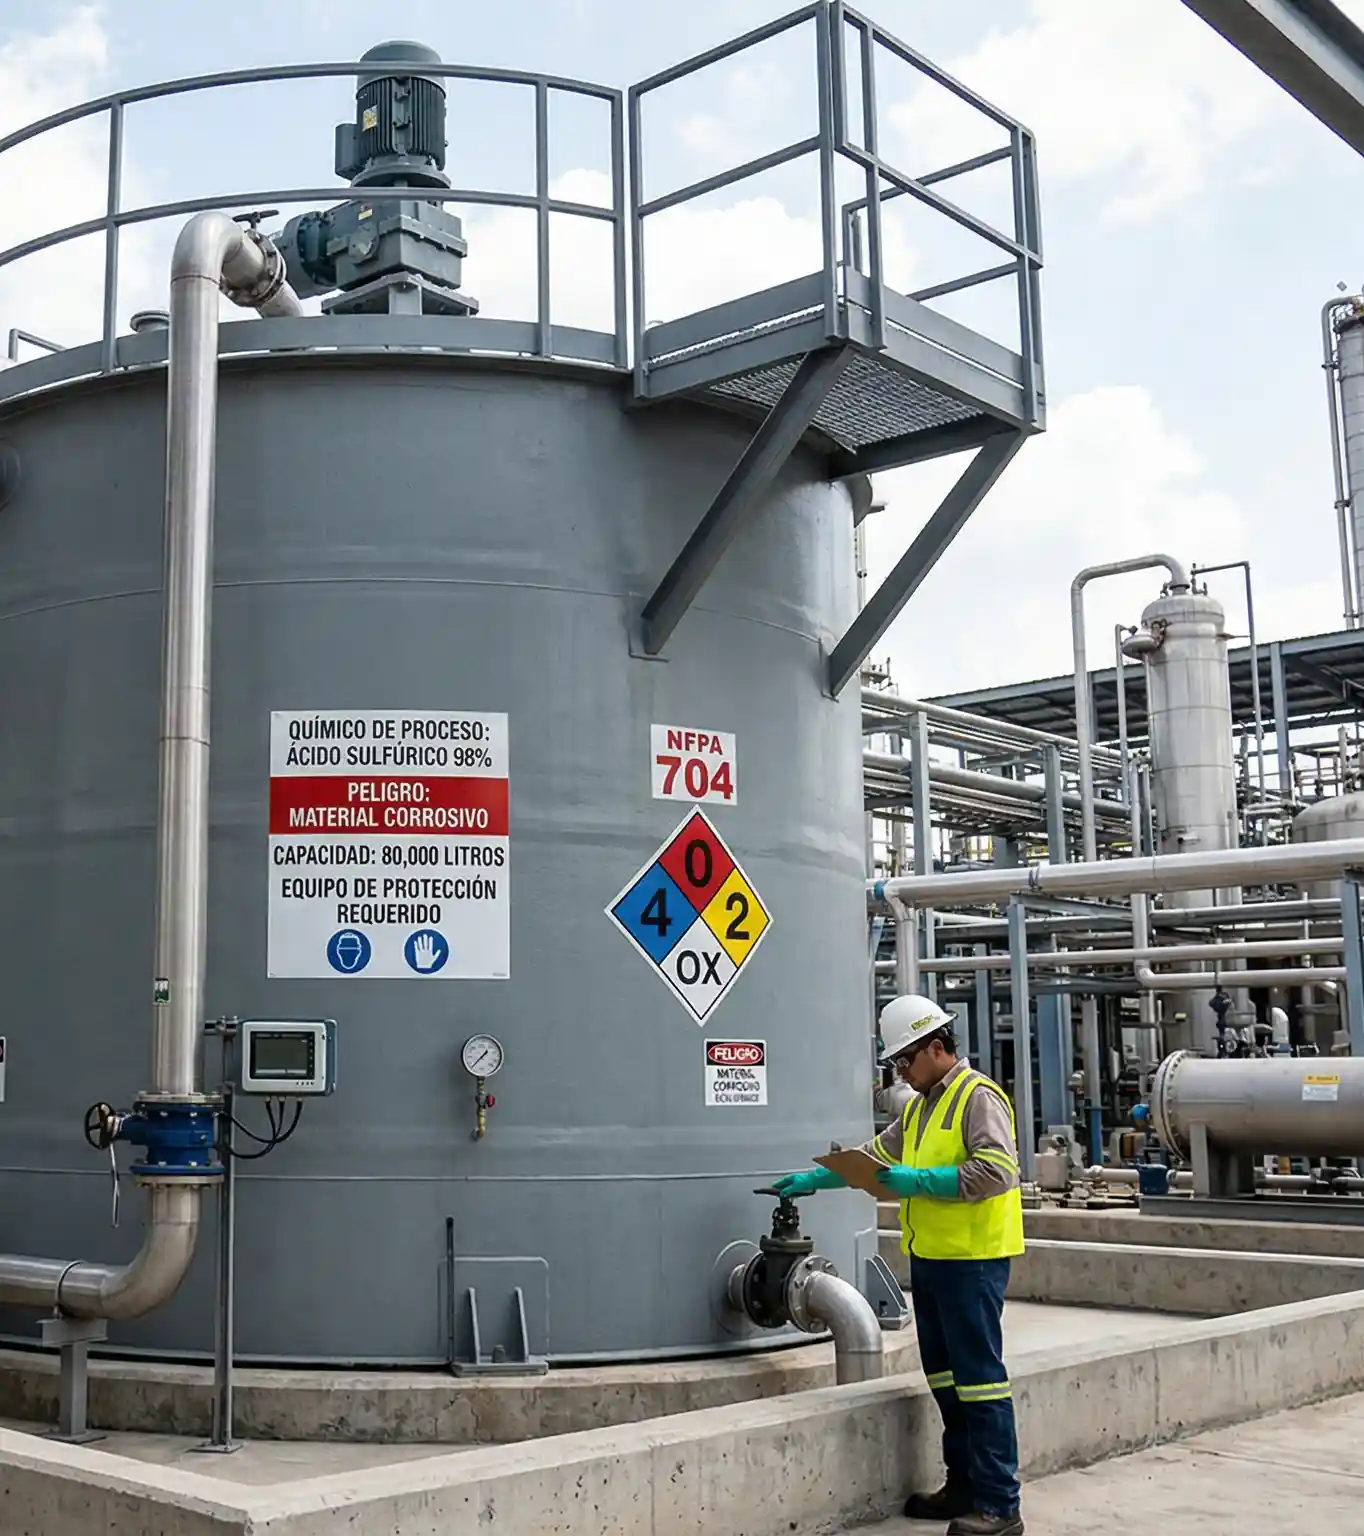
chemical tank industry
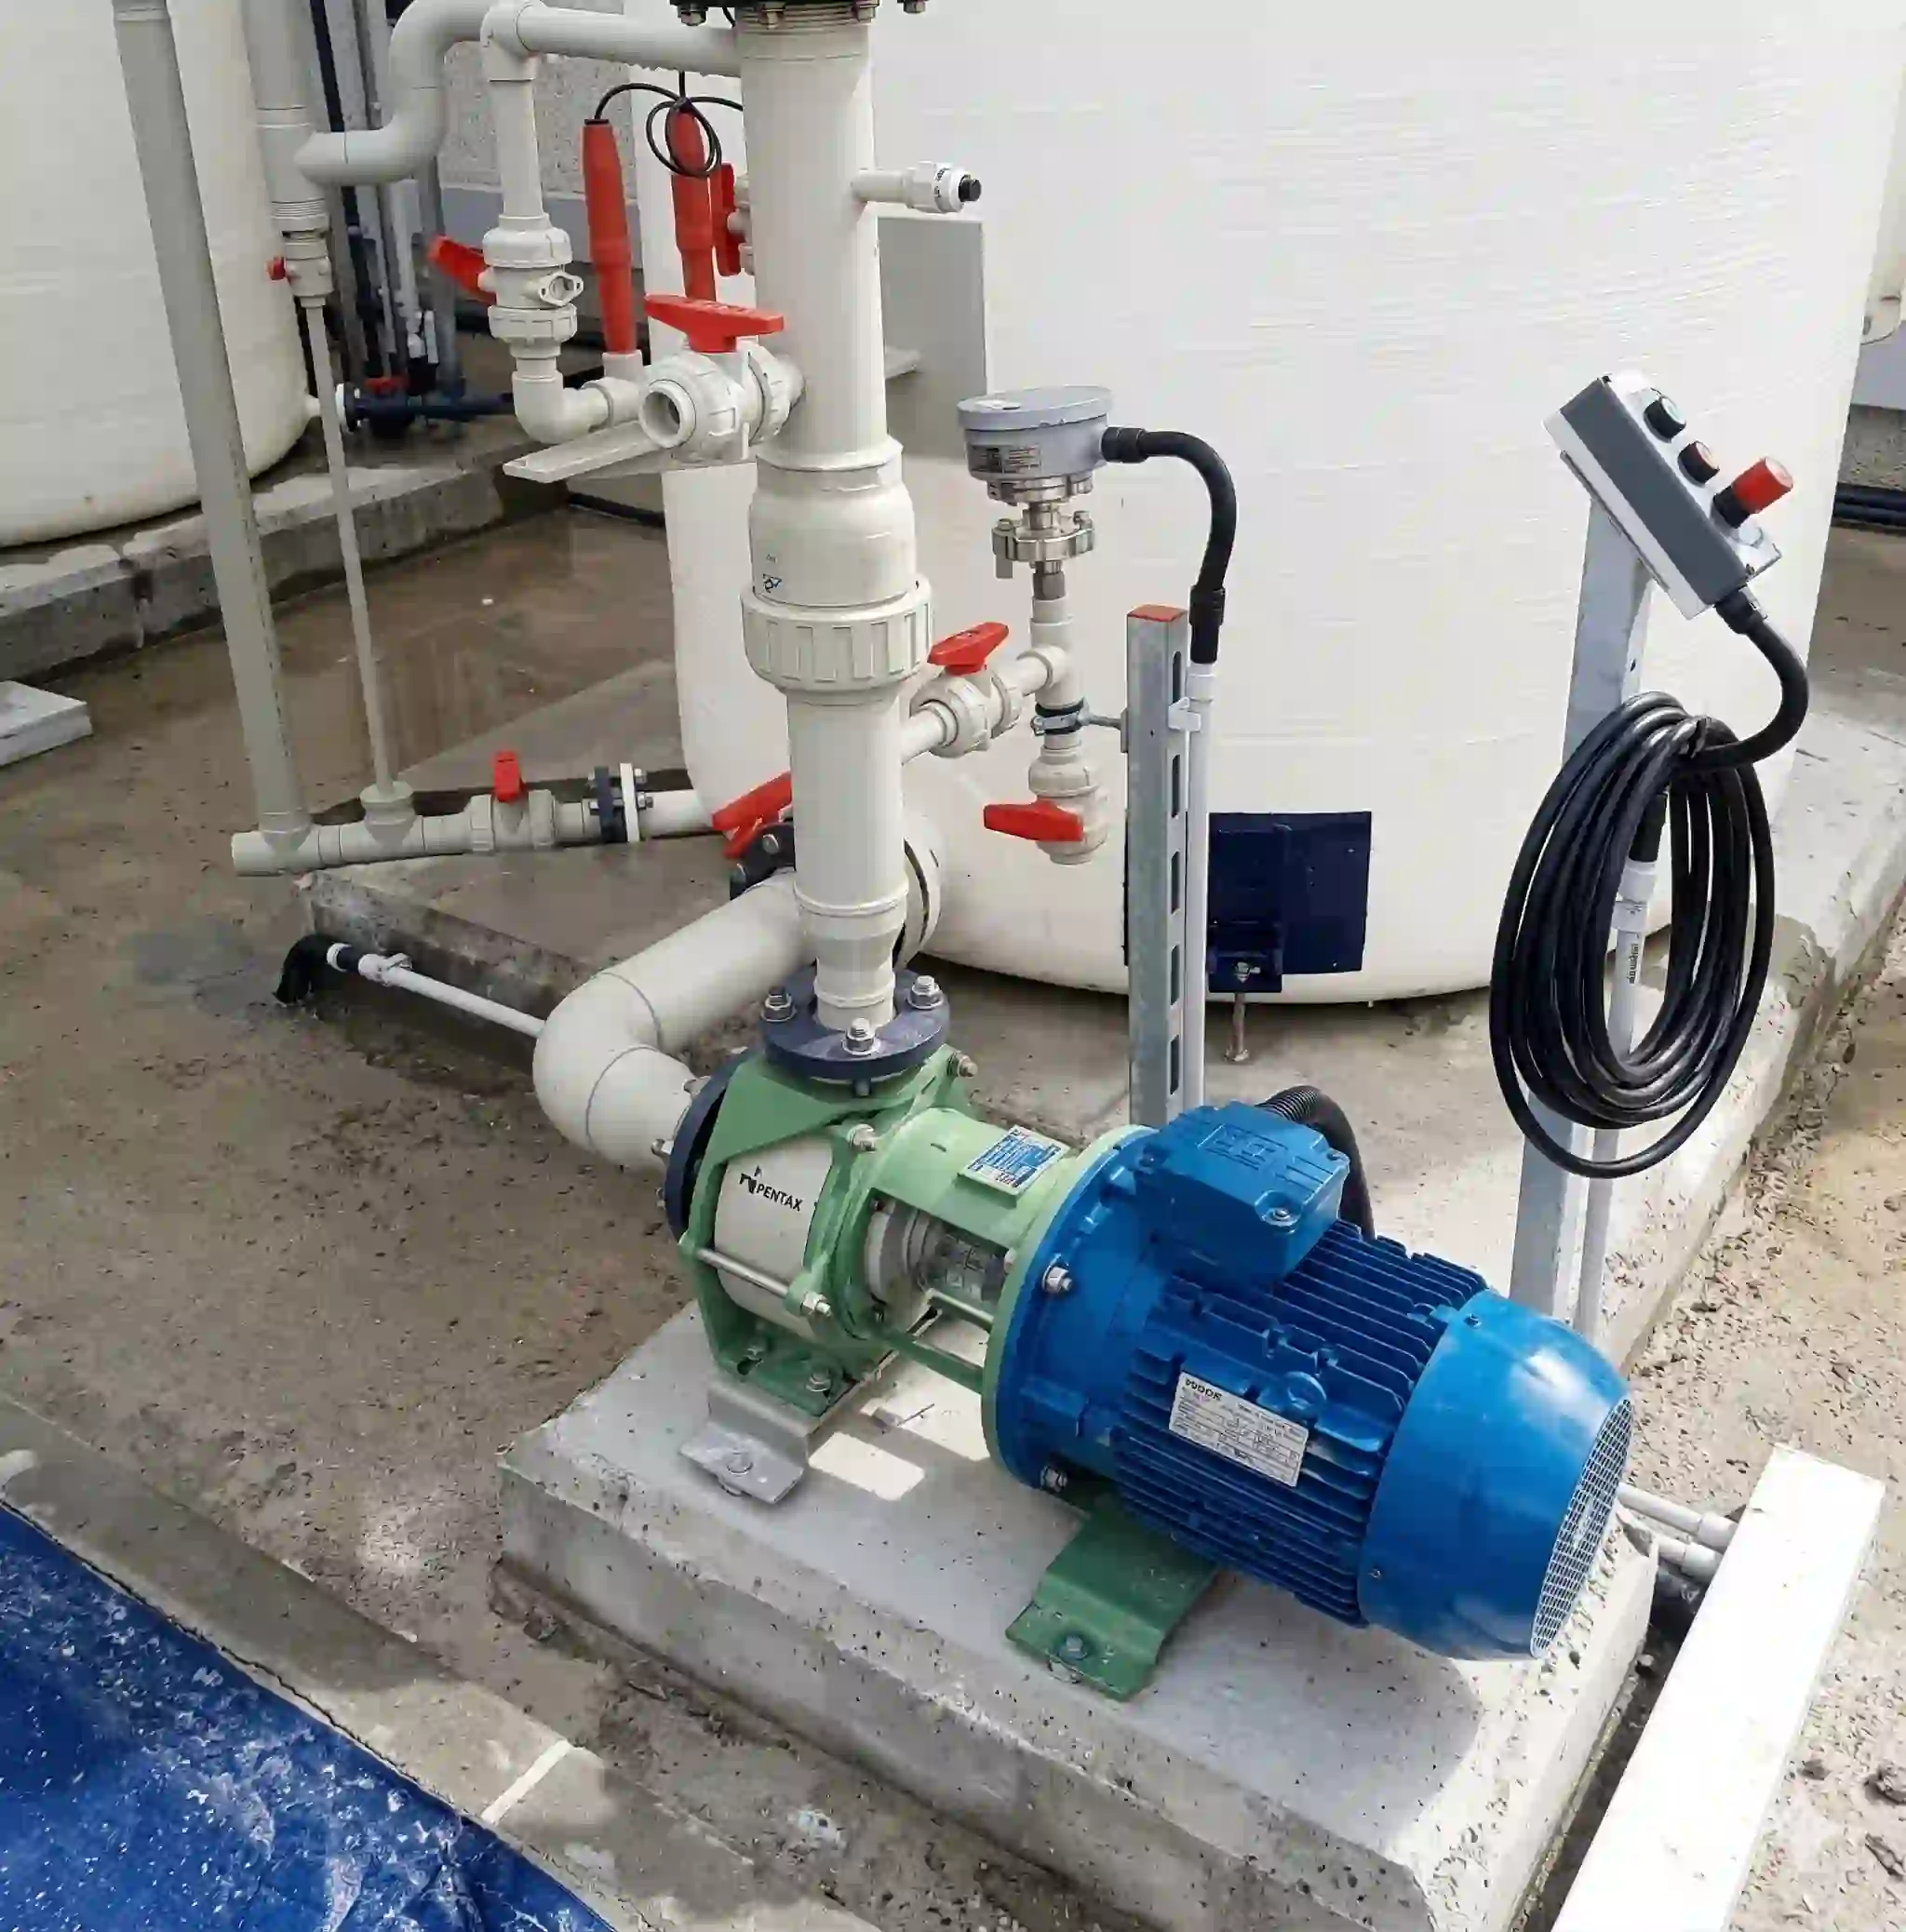
chemical industry pump

Industrial grade reliability

Key advantages for chemical manufacturing

  • Absolute corrosion resistance: Solid thermoplastic construction eliminates the risk of metallic degradation when handling strong acids and alkalis.

  • Heavy-duty continuous operation: Engineered for maximum mechanical durability and reliability in demanding 24/7 chemical processing environments.

  • Standardised integration: Designed in strict compliance with ISO 2858 and EN 22858 standards for seamless and standardized plant integration.

  • Hazardous area compliance: Fully ATEX-certified configurations available to guarantee maximum safety in potentially explosive atmospheres.

High-performance equipment

Recommended pumping solutions for the chemical industry

Explore our range of heavy-duty thermoplastic pumps, engineered to withstand extreme corrosion and ensure reliable continuous operation in chemical processing plants.

Ideal for handling highly toxic or aggressive chemical compounds.

These sealless magnetic drive pumps ensure total fluid containment and zero emissions, providing maximum environmental safety in heavy chemical processing.

Standardised heavy-duty centrifugal pumps compliant with EN 22858 and ISO 5199.

Machined from solid thermoplastic blocks, they offer exceptional resistance to severe corrosion in continuous industrial operations.

Compact and highly efficient monobloc pumps perfect for chemical installations with limited space.

The direct-coupled design eliminates the need for shaft alignment while maintaining excellent resistance to aggressive reagents.

Featuring a glandless overflow design without mechanical seals, these pumps excel at handling corrosive effluents and chemical slurries with suspended solids. They also offer excellent dry-running capabilities.

Engineered with a robust cantilevered shaft to pump aggressively corrosive liquids directly from process sumps and tanks.

They provide complete dry-running safety and are essential for industrial wastewater management.

Frequently asked questions about our pumps for chemical industry

Metallic pumps, even those manufactured from high-grade stainless steel or exotic alloys, are highly susceptible to rapid corrosion when exposed to aggressive industrial acids, alkalis, and strong solvents.

This chemical attack inevitably leads to mechanical failures, frequent maintenance interventions, and costly unplanned downtime. Thermoplastic pumps, machined directly from thick, solid blocks of PP, PVDF, or E-CTFE, completely eliminate the inherent risk of metallic corrosion and structural degradation.

By utilising these advanced, chemically inert materials, we guarantee total resistance against the most severe corrosive fluids, ensuring your pumping systems remain fully operational under extreme conditions.

Furthermore, the solid plastic construction provides exceptional mechanical stability and a significantly extended service life when compared to lined or coated metal alternatives, ultimately protecting your process continuity and reducing your total cost of ownership.

Handling fluids that are both highly corrosive and abrasive is one of the greatest challenges in heavy chemical manufacturing. Standard centrifugal pumps often suffer from rapid seal wear under these harsh conditions, leading to hazardous leaks and catastrophic mechanical failures.

To solve this, our vertical external pumps (BHS/BXS series) feature a glandless overflow design that entirely eliminates vulnerable mechanical seals and delicate internal wear rings. This innovative construction removes the components most susceptible to abrasive wear, making them highly resistant to suspended particles, sludge, and industrial effluents.

Additionally, this unique design allows the equipment to run dry indefinitely without sustaining any thermal or mechanical damage, providing unmatched reliability in demanding applications such as sump drainage, waste treatment, and continuous slurry transfer.

In heavy chemical processing, preventing the leakage of toxic, flammable, or aggressive fluids is an absolute priority to ensure plant safety and environmental compliance. Traditional mechanical seals are the most common point of failure, often leading to dangerous emissions and hazardous working conditions.

For these critical applications, we strongly recommend our sealless magnetic drive pumps (BKM series). These advanced pumps utilise a hermetic thermoplastic isolation shell that completely replaces the mechanical seal, transmitting the motor’s driving torque through a powerful, synchronized magnetic coupling.

This sealless technology guarantees absolute fluid containment and zero fugitive emissions into the surrounding environment, ensuring the maximum protection of your plant personnel and maintaining strict compliance with international environmental and safety regulations.

Chemical manufacturing plants frequently involve the handling of highly volatile solvents, combustible liquids, and flammable gases, creating environments where the risk of ignition must be absolutely minimized. Safety is paramount in these zones, and standard pumping equipment is often unsuitable.

To address this, our heavy-duty thermoplastic pumps can be supplied with comprehensive ATEX certification for safe operation in classified hazardous zones. We achieve this by adapting our standard equipment with specialised, electrically conductive plastic compounds and certified explosion-proof electric motors.

This careful engineering prevents the dangerous accumulation of static electricity and eliminates the risk of sparking, ensuring your production facility meets the highest international safety directives while maintaining the exceptional chemical resistance required for your process.

Plant engineers require equipment that not only performs reliably but also integrates easily into existing piping infrastructure without requiring costly or complex modifications. To guarantee maximum compatibility and ease of installation, our heavy-duty process pumps are designed and manufactured in strict compliance with the most demanding global engineering criteria.

They strictly adhere to international dimensional and performance standards, including ISO 2858, EN 22858, and ISO 5199. This critical standardisation guarantees seamless integration into your current plant layouts, allowing for direct drop-in replacements of older, failing metallic pumps.

Ultimately, adhering to these rigorous engineering guidelines ensures long-term mechanical reliability, optimal hydraulic efficiency, and greatly simplified maintenance procedures across your entire industrial facility.

Get in touch today

Receive your free quote