Mineral extraction and processing

Heavy-duty pumps for the mining industry

Engineered to reliably handle highly abrasive ore slurries and aggressive leaching acids,
guaranteeing maximum uptime in extreme hydrometallurgical environments.

Hydrometallurgical processing

Reliable fluid transfer for abrasive ore slurries

The extraction and refinement of minerals involve some of the most destructive fluids on the planet. Pumping highly abrasive ore slurries and concentrated leaching acids, like those used in copper or gold recovery, quickly destroys standard metallic equipment through a brutal combination of severe erosion and chemical attack.

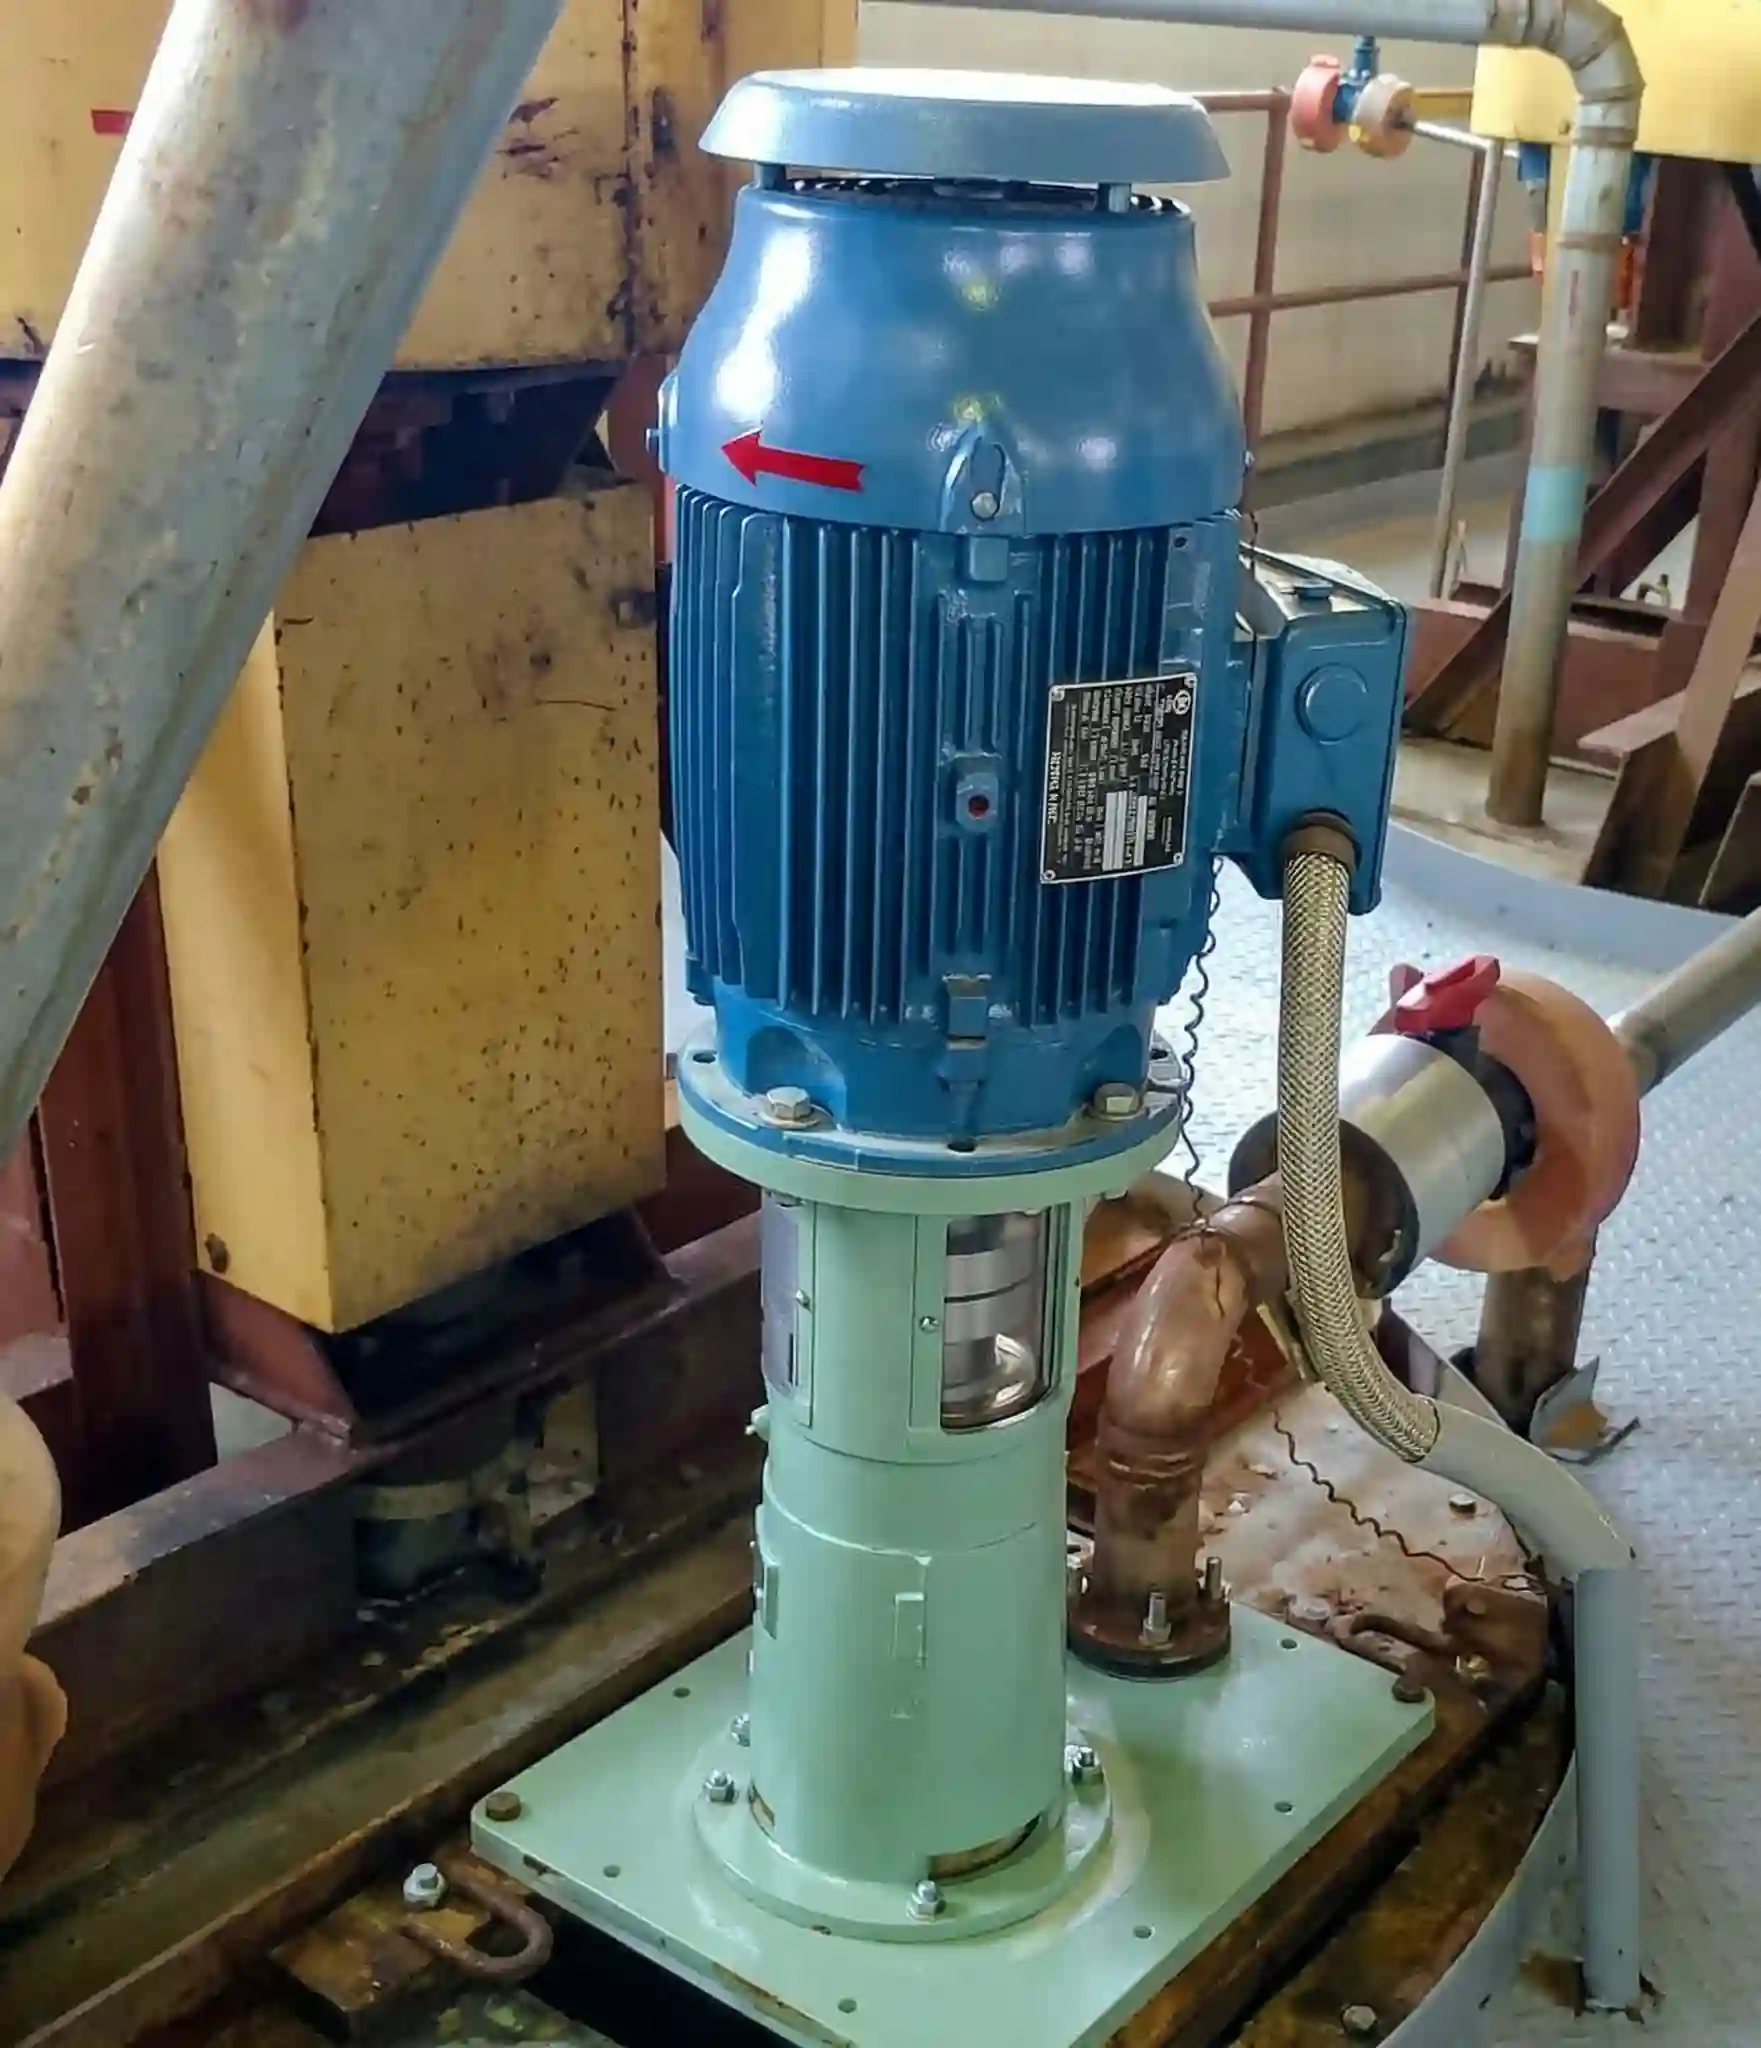
Tecnium Pumps provides ultra-durable thermoplastic solutions built specifically to survive these punishing mining environments. Utilizing massive solid-block polymers and specialized glandless designs, our pumps deliver unmatched wear resistance and continuous operational stability, ensuring your mineral processing circuits keep running safely even under extreme mechanical stress.
mining industry pump

Engineered for extreme extraction

Core advantages for mining operations

  • Extreme abrasion resistance: Heavy-duty thermoplastic hydraulics and open impeller designs effortlessly handle dense, particle-laden ore slurries without clogging or rapid internal wear.

  • Immunity to leaching acids: Solid plastic construction provides absolute protection against the aggressive sulfuric acids and cyanide solutions used in modern hydrometallurgical recovery.

  • Dry-running sump capabilities: Cantilevered vertical configurations feature no submerged bearings, allowing for safe and continuous drainage of unpredictable mine dewatering pits.

  • Reduced maintenance downtime: Glandless sealing architectures eliminate vulnerable mechanical seals, preventing frequent fluid leaks and costly pump failures in remote processing plants.

Heavy-duty extraction equipment

Recommended pumping solutions for the mining industry

Explore our rugged selection of thermoplastic pumps, specifically engineered to withstand extreme abrasion, heavy ore slurries, and highly corrosive leaching acids in remote mineral processing plants.

Essential for dewatering unpredictable mine pits and draining aggressive tailing sumps. The robust cantilevered design features no submerged bearings, enabling safe, continuous dry running while transferring heavy mineral-laden water without mechanical wear.

The ultimate choice for circulating abrasive slurries and concentrated metal leaching solutions. Engineered with an advanced glandless architecture, these units completely eliminate mechanical seals, providing exceptional reliability and leak-free operation when handling particle-rich mining fluids.

Built for massive hydrometallurgical processing stages and continuous acid transfer. Manufactured to standardized EN 22858 and ISO 5199 dimensions, these solid thermoplastic block pumps deliver unmatched resistance against the severe chemical attack of sulfuric acid and cyanide.

A space-saving and highly efficient solution for auxiliary chemical dosing within compact mineral recovery skids. This monobloc configuration provides outstanding chemical resistance without requiring complex mechanical alignments in challenging, space-restricted mining environments.

Frequently asked questions about our pumps for the mining industry

Pumping crushed rocks and heavy mineral slurries causes severe internal erosion in standard metallic pumps. The constant scouring action wears down impellers and casings, leading to a rapid decline in hydraulic efficiency and frequent mechanical breakdowns.

Our heavy-duty pumps are engineered with ultra-thick solid thermoplastic components and optimized open impellers. This specialized internal geometry allows dense, abrasive particles to pass through the fluid path without causing destructive friction or clogging.

By maintaining their structural integrity against severe mechanical wear, these units significantly extend the mean time between failures, ensuring your mineral extraction circuits remain highly productive with minimal maintenance downtime.

Hydrometallurgical recovery methods rely on devastatingly corrosive chemicals, such as concentrated sulfuric acid for copper and sodium cyanide for gold. These leaching agents quickly dissolve standard metal alloys and destroy conventional pump seals.

To counter this extreme chemical attack, our pump casings are machined from massive blocks of virgin polymers like PP and PVDF. These non-metallic materials are inherently immune to the acidic and caustic solutions used in mineral processing.

This total chemical resistance guarantees safe and continuous fluid transfer during critical recovery stages, completely eliminating the risk of hazardous leaks and protecting both plant personnel and the surrounding environment.

Mine dewatering sumps and tailing collection pits often experience rapid fluctuations in fluid levels. Standard submersible pumps frequently suffer catastrophic bearing failures when they accidentally run dry during these unpredictable drainage cycles.

Our vertical cantilever sump pumps are designed with a heavy-duty shaft architecture that requires no submerged bottom bearings. The entire rotating assembly is safely supported above the mounting plate, entirely outside the corrosive fluid.

Because there is no physical contact within the wet end, these resilient units can operate without fluid indefinitely without suffering frictional heat or breakdown, offering absolute peace of mind for automated mine dewatering systems.

The primary point of failure in slurry pumping is the mechanical seal. Abrasive particles inevitably penetrate the seal faces, causing rapid grinding wear, severe fluid leakage, and costly damage to the pump shaft.

Our vertical external pumps utilize an innovative glandless architecture that completely removes mechanical seals from the equipment design. A dynamic hydrodynamic seal prevents fluid escape while the pump is running, without any physical contact between surfaces.

This seal-less configuration allows the pump to effortlessly handle heavy, particle-laden slurries without leaking or wearing out, drastically reducing spare parts consumption and maintenance labor in remote mining locations.

Upgrading failing equipment in remote mining facilities can be a logistical nightmare, especially if the new pumps require extensive modifications to existing concrete foundations or piping networks to fit properly.

To facilitate hassle-free upgrades, our heavy-duty process pumps comply with established global dimensional norms, including the ISO 5199 and EN 22858 standards. This standardization ensures our thermoplastic units perfectly match the footprint of traditional metallic pumps.

This precise physical matching enables a direct plug-and-play installation during scheduled maintenance windows, allowing remote extraction sites to transition to durable plastic pumps without modifying existing pipework.

Get in touch today

Receive your free quote